 Inside the Asset
Mike brings hands-on inspection experience to his work with unmanned systems at MFE Inspection Solutions in Chicago. A former multi-certified Level II inspector and nuclear quality-control professional, he has worked in refineries, chemical plants, nuclear facilities, food and biofuel facilities, and steel manufacturing.
Here, he explains how he approaches Elios 3 assignments, why remote ultrasonic thickness measurements still depend on inspection judgment, and what a final visual sweep can reveal before an asset returns to service.
This interview has been edited and condensed for clarity and approved by Mike for publication. Answers describe his experience; editorial notes are separate. Mike works for MFE Inspection Solutions, a Flyability partner.

Experience and applications
What drew you to the Elios 3?
Mike: I now work with MFE Inspection Solutions as the Unmanned Ground Robotics Product Line Manager and serve as a technology advisor to the clients I consult. Our team has been partnered with Flyability since around 2017, when we were introducing the Elios 1 to industries across the U.S. market. The Elios 3 is the latest version of that indoor aircraft that our team is working with.
My background before this role was very hands-on. I was a multi-certified Level II inspector and nuclear QC, with experience in oil and gas refineries, chemical plants, nuclear power plants, food and biofuel facilities, and steel manufacturing. A lot of that work involved entering confined spaces or work at heights to perform nondestructive examinations of welded connection points and visual evaluations.
Where have you used the Elios 3?
Mike: I have performed visual and thermal inspections and captured ultrasonic thickness data inside confined-space assets including above-ground storage tanks, knockout drums, surge drums, bullet tanks, flare stacks, boilers, and more.
I have also inspected pressure vessels and other industrial equipment containing components such as bolted connections, agitator blades, temperature probes, baffles, and spray-ball cleaning nozzles.
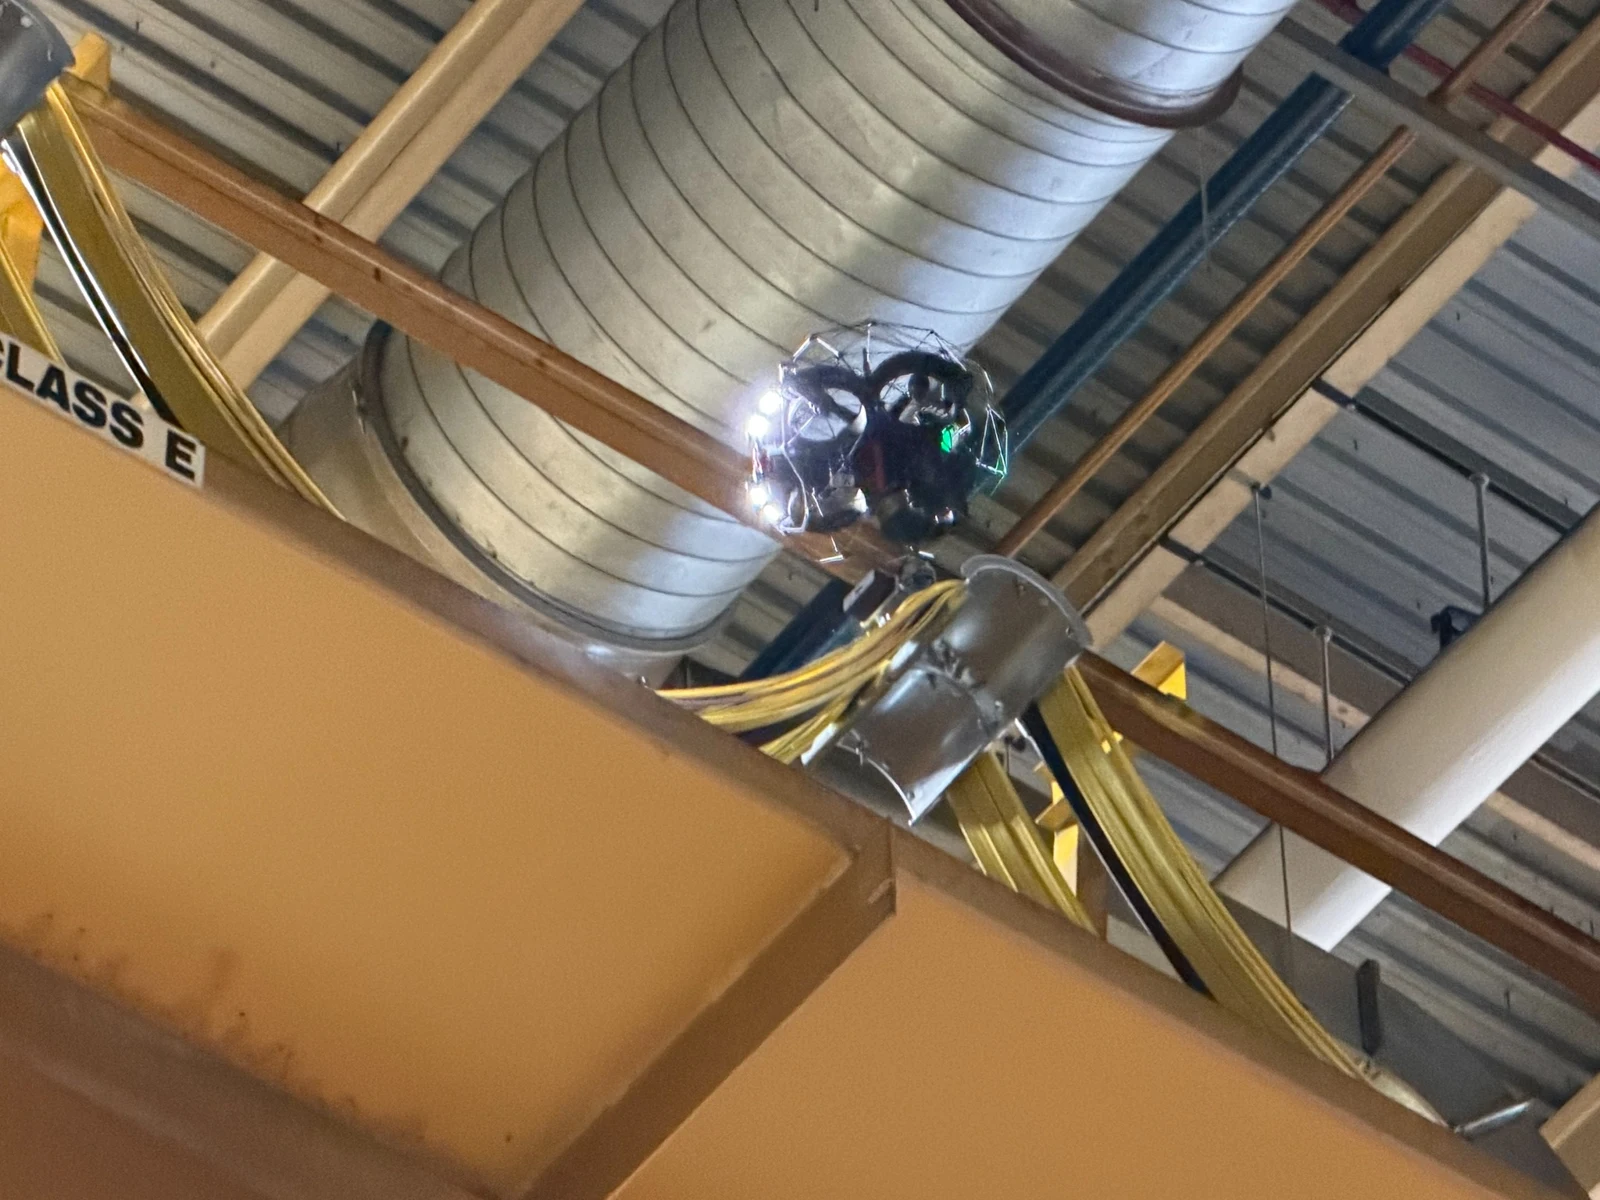
Outside industrial plants, I have used the equipment for visual and thermal inspections of underground water, sewer, and combined utility systems, large-diameter culverts, electrical vaults, hydroelectric penstocks, and underground maintenance pits. Indoors but outside confined spaces, I have used it to inspect cranes, crane rails, overhead piping systems, and overhead rigging.
Qualifying the job and planning the flight
How do you determine whether the Elios 3 is appropriate for a particular job?
Mike: It starts by understanding what the end user actually needs. Are they looking for a general condition assessment, an API-related inspection, a coating-warranty check, or investigating a suspected blockage? Those objectives drive the inspection plan.
We are very technology-centric and advocate for remote visual inspection where it can provide the required information while minimizing human exposure to confined-space and work-at-height hazards. It can also reduce the need for scaffolding and potentially reduce downtime.
Then we qualify the environment. Industrial facilities have their own permitting processes, and the equipment has to be appropriate for those conditions. We also look at physical access, asset geometry, material construction, signal coverage, and the areas the client needs us to reach.
The bigger point is that you need to ask the right questions before committing to a tool.
What do you do before arriving on site?
Mike: A lot of our pre-check work happens the week before.
We conduct several flights to make sure the aircraft is in good, airworthy condition and, when possible, simulate some of the conditions we expect to encounter. We install and test the payloads we expect to use and confirm that everything is updated and functioning.
The pilot also makes sure the drone batteries, remote controller, and tablet are charged so the system is ready when we arrive.
What mistakes should newer pilots avoid?
Mike: The first mistake is failing to properly qualify the application.
Ask enough questions up front to understand exactly what data the customer needs. That gives everybody a better chance of success.
The second is trying to accomplish too many objectives during one flight. Plan each flight around a defined goal. If the objective is to document hardware connections, concentrate on that. If you need high-quality point-cloud coverage for post-review localization, plan a flight path that supports that objective.
Proper planning prevents poor performance.

Collecting and interpreting thickness data
What does setup look like for ultrasonic-thickness work?
Mike: Once the UT payload is installed and the aircraft is powered on, the pilot goes through the pre-flight checklist. That is a final opportunity to verify that the hardware is seated properly, the couplant is feeding through the line, and spare cable length is secured.
We then go into the UT settings and perform a two-step calibration. We use a NIST-traceable calibration block matching the asset material we intend to capture thickness readings on.
The inspector can adjust parameters such as measurement range and grid width as required. Probe selection depends in part on anticipated material and coating thickness, and a trained UT inspector needs to understand when to use single-echo versus echo-to-echo techniques and how to evaluate the live waveform.
How important is location accuracy when collecting UT readings?
Mike: Very important.
Inspectors are often working from plant drawings, isometrics, P&IDs, and previous inspection records. Translating a two-dimensional drawing into an exact three-dimensional inspection location can introduce human error.
Previous CMLs may be identified by compass locations such as north, east, south, and west, or eight-point orientations. Sometimes old couplant marks are still visible, which can help an inspector return more closely to the same location.
Surface condition matters too. If corrosion, debris, or oxidation prevents good coupling, some level of surface preparation may be necessary. The Elios 3 UT cleaning module can address certain lighter surface conditions, while heavier corrosion or other circumstances may require another unmanned system or traditional hands-on preparation.

How do you distinguish a meaningful UT result from a misleading one?
Mike: Training and context matter.
One example from my broader UT experience, not an Elios 3 inspection, involved an in-service piping elbow at an oil and gas refinery. We were using an Olympus 38DL with a D790 transducer. The reading was moving between 0.252 inch and 0.126 inch, but we were getting a good response at 0.126 inch.
The prior inspection, about 12 months earlier, had reported nearly twice that thickness. That kind of apparent wall loss warranted additional scrutiny. Our inspection team believed the lower reading was correct and suspected the prior result may have involved ultrasonic 'doubling,' where a gauge reports approximately twice the actual thickness.
A radiographic technician was brought in to perform digital radiography, which confirmed the 0.126-inch measurement.
The lesson is that an inspector has to use the waveform, calibration, inspection history, material condition, and other available information rather than accepting a number without context.
Editor’s note: This case describes a separate handheld UT inspection. It is not an Elios 3 UT result.
Visual screening and equipment selection
How do you use the Elios 3 for visual inspections beyond formal code work?
Mike: It is very useful as a rapid screening tool before and after confined-space entry.
Before entry, the aircraft can help answer practical planning questions: How much scaffolding might be needed? Are repairs likely? How many areas appear to require attention? Is there something inside the asset that nobody anticipated?
That information can help a maintenance team plan the next step before sending people into the space.
We also use it for post-entry visual sweeps. We have experienced several instances where an asset was believed ready to return to service, but a final drone inspection found items such as a work glove, scaffold footing, or loose hardware still inside.
Something that looks minor can create significant consequences once equipment returns to operation.
What are the Elios 3's limitations?
Mike: Every application is different. If the aircraft cannot physically fit through the available entryway, we may move to an industrial crawler, a pan/tilt/zoom camera system, or a handheld videoscope.
One of our advantages at MFE is access to many different inspection technologies. We need to understand the application and select the equipment that best addresses it.
Data review and equipment care
How do you review and communicate the inspection data?
Mike: The pilot creates the asset folders on site. Flights within the same asset can be localized together, allowing the pilot to build out the captured environment while viewing point-cloud information during the mission.
Afterward, flight recordings saved to the tablet can be reviewed to confirm that required visual data was captured.
When we import the project into Flyability's Inspector software, the asset names and flights carry over. One thing I have always credited Flyability with is making complex datasets easy for users to understand. Depending on the required deliverable, users can display or remove different information layers, produce reports, and share data through the available expanded software environment.
How do you care for the aircraft after a job?
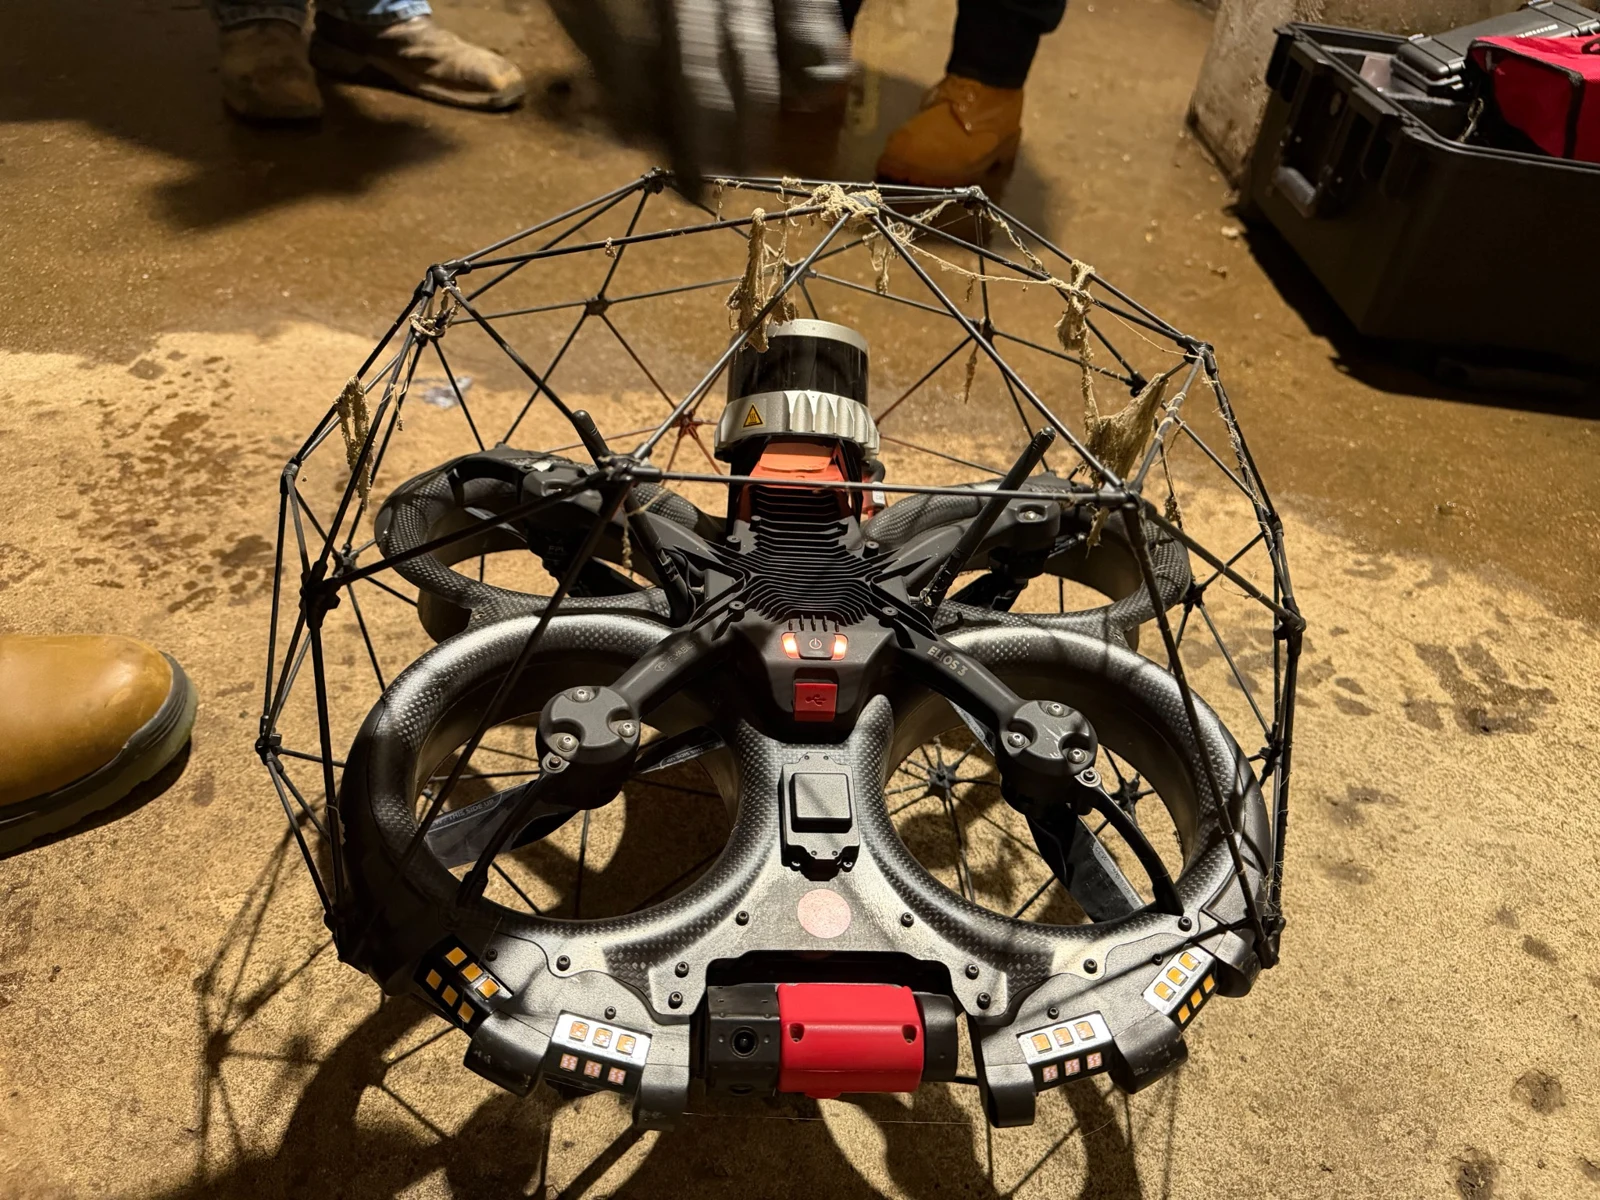
Mike: We remove accumulated dust and debris between flights and at the end of the day, paying attention to the motors and LED panels. Cleaning methods need to follow manufacturer guidance because some products may affect onboard components.
Everything is then packed into its supplied transport cases. After returning to the office, we place batteries into the appropriate storage state based on their condition and use.
What is your most valuable advice for someone starting with the Elios 3?
Mike: You will get out of this what you are willing to put into it.
Think of the Elios 3 as a very capable extension of your eyes, with the added benefit of better deliverables while allowing you to keep your feet on the ground.
Confined spaces and work at height carry known risks. Where appropriate, this equipment can reduce the number of human entries and exposures required. That depends on properly qualifying the application, planning the mission, and having trained people operate and interpret the equipment.
At MFE, our team trains users on the equipment and remains available as a resource when additional questions or repair needs come up.
Practical takeaways
- Qualify the application first. Define the required information, access, environment, asset geometry, and deliverable before selecting equipment.
- Give each flight a clear objective. Visual documentation, UT measurements, and point-cloud coverage can call for different flight plans.
- Interpret the measurement. Calibration, surface condition, waveform evaluation, and inspection history matter when deciding whether a UT reading is meaningful.
- Keep other tools available. A crawler, PTZ camera, videoscope, or hands-on method may better suit the application.
- Include equipment care and data organization in the job. The inspection is only useful if the findings can be reviewed and understood.
About Mike
Mike Vanovermeir is the Unmanned Ground Robotics Product Line Manager for MFE Inspection Solutions in Chicago. His background includes confined-space nondestructive examination, nuclear quality control, and the application and training of unmanned inspection technologies. He also supports client proof-of-concept demonstrations and equipment training.